
Electrostatic Powder Coating Booths
Powder coating contains no solvent: there are no volatile organic compound emissions, and most of the powder that does not reach the surface can be recovered. These two properties markedly reduce both environmental load and material cost compared with wet paint.
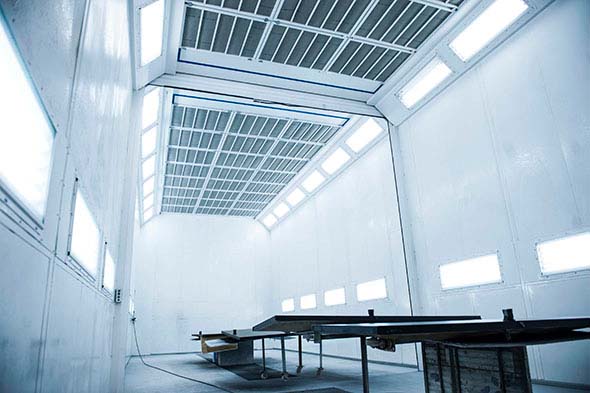
How the process works
The powder is charged electrostatically, sprayed onto the earthed part and held on the surface by electrical attraction. Powder that misses the part is extracted inside the booth, separated in a cyclone, screened and returned to the feed system. Recovery efficiency is the main variable determining the economics of the system.
Colour change is the most critical operating issue in powder coating. The booth, cyclone and feed lines must be completely cleared of the previous colour. Quick colour-change booths are designed to shorten this time; on lines with frequent colour changes the difference in initial investment pays back quickly.
Curing is the stage where the powder melts into a film and cures chemically. Insufficient curing directly reduces the mechanical and chemical resistance of the coating; thermal profile measurement is therefore part of acceptance.
Technical framework
| Application | Electrostatic · automatic and manual guns |
|---|---|
| Recovery | With cyclone + filter unit |
| Colour change | Quick colour-change booth option |
| Curing | Metal temperature and time per the paint data sheet |
The figures are typical operating ranges for the sector. Every line is recalculated according to part geometry, target capacity, paint system and customer specification.
Related topics
Let’s arrange a preliminary technical discussion for a powder coating line. Share your part dimensions, target capacity and paint system, and our process engineer will prepare an outline concept and budget range.