
Plastics Paint Shop System
Plastic differs from metal in three ways: its surface energy is low, its thermal tolerance is limited, and its dimensional stability degrades with temperature. These three constraints explain why plastics lines are laid out differently from metal lines.
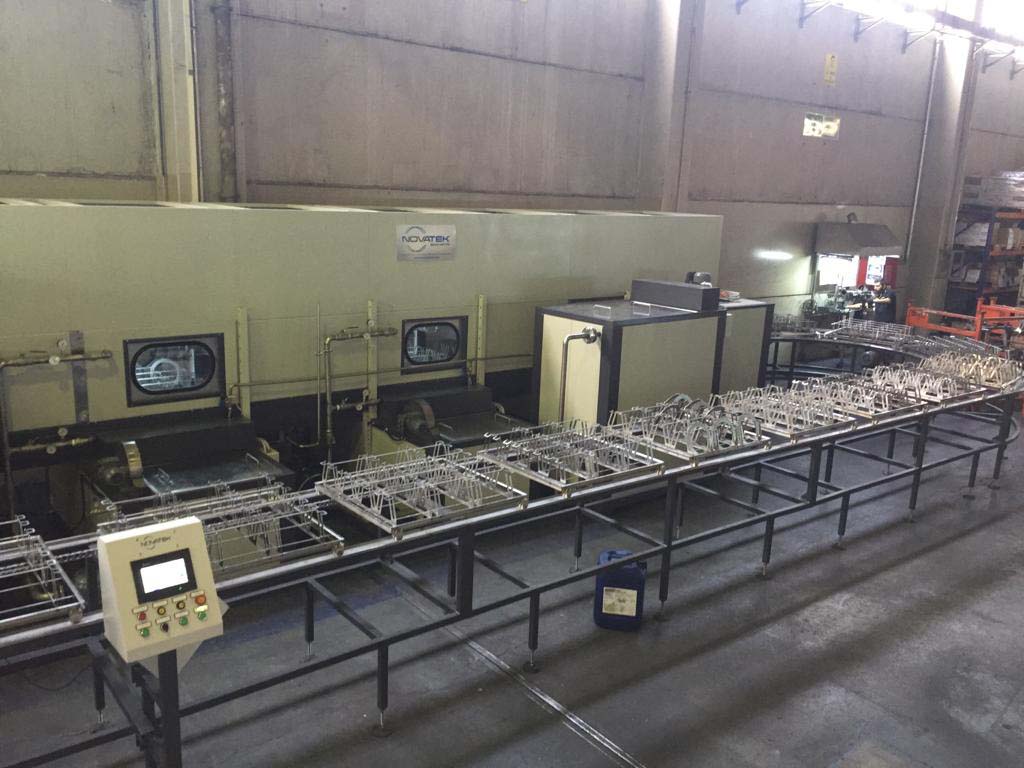
How the process works
For paint to adhere to plastic, surface energy must be raised. Flame treatment or plasma treatment achieves this. The effect is not permanent; an activated surface reverts within hours, so the interval between pretreatment and painting is a process parameter.
Plastic parts do not withstand high temperature as metal does. Drying is typically below 80 °C, IR-assisted and short. The oven temperature must stay below the material’s heat deflection temperature.
Colour stability depends directly on booth climate. Fluctuations in humidity and temperature create shift-to-shift colour differences, particularly with metallic and pearlescent paints. Plastics booths therefore run under humidity and temperature control from an air handling unit.
Technical framework
| Booth climate | 23 ± 2 °C · 60 ± 5 % relative humidity |
|---|---|
| Pretreatment | Flame treatment · plasma |
| Drying | IR-assisted, low temperature |
| Application | Robotic · electrostatic suitability depends on the part |
The figures are typical operating ranges for the sector. Every line is recalculated according to part geometry, target capacity, paint system and customer specification.
Related topics
Let’s arrange a preliminary technical discussion for a plastics paint shop system. Share your part dimensions, target capacity and paint system, and our process engineer will prepare an outline concept and budget range.