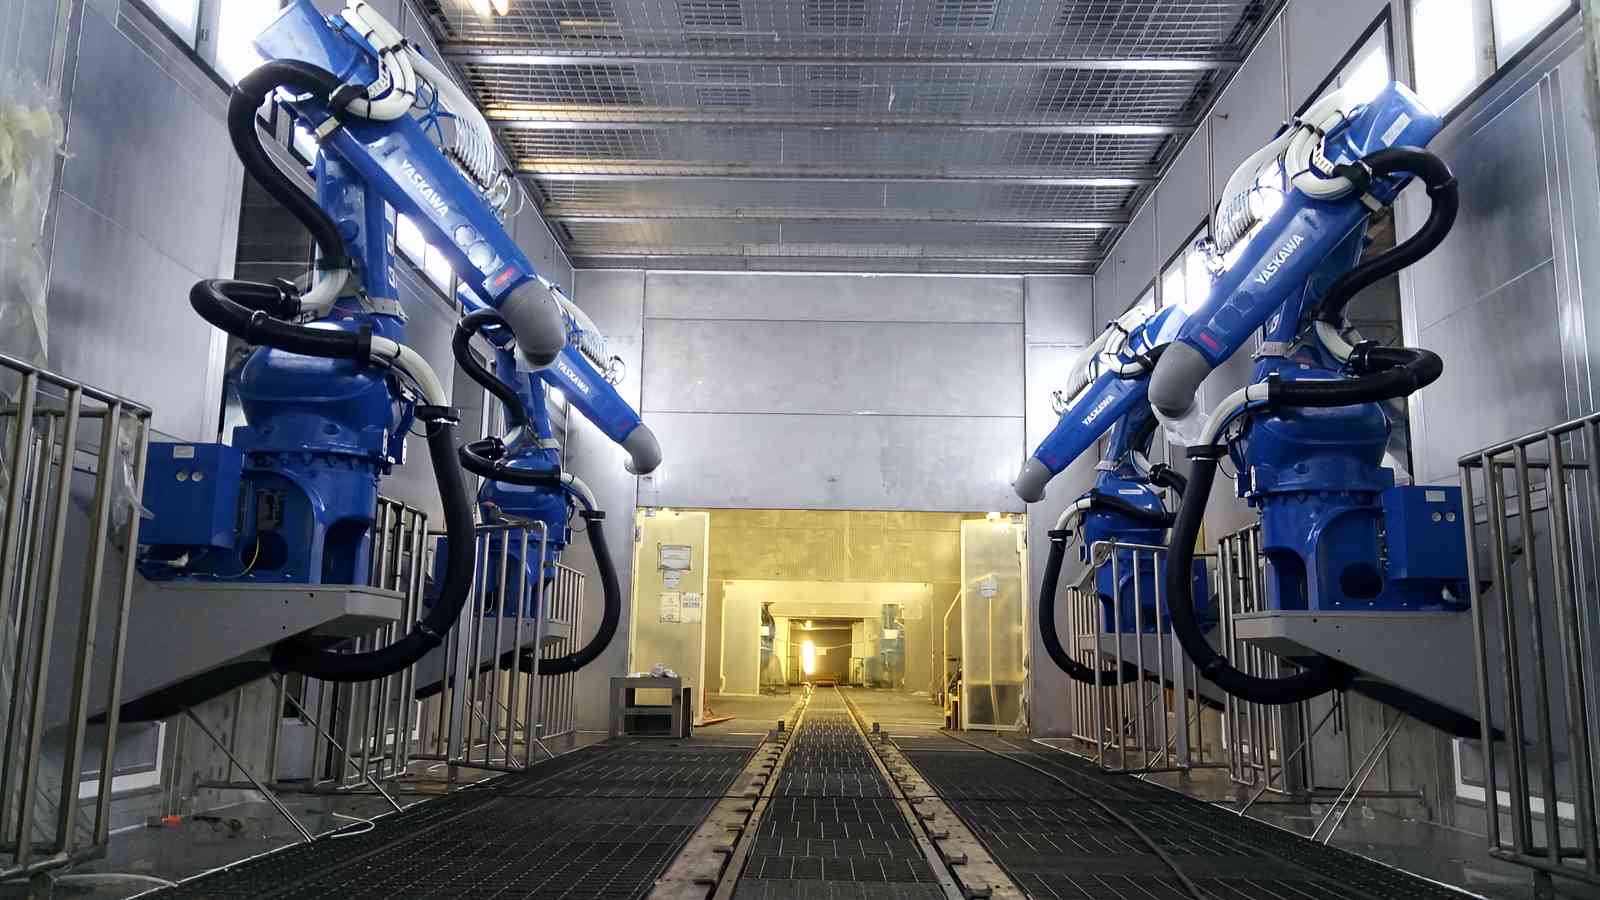
Automated Painting Robots
The real gain from a robot is not speed but repeatability. An experienced operator does good work, but not the same work at the end of a shift, on a different day, or once they leave. Properly programmed, a robot applies to every part from the same distance, at the same speed and at the same flow rate.
How the process works
A robot cell is built in three layers. Mechanical layer: the robot’s reach envelope, the position of the part and the gun trajectory. Process layer: flow rate, atomising pressure, electrostatic voltage and the colour change system. Safety layer: perimeter guarding, interlocked doors, area scanners and emergency stop circuits.
Adding a robot to an existing line (brownfield integration) is a different problem from building a line from scratch. Booth dimensions, conveyor speed and electrical infrastructure are already fixed; the robot is placed within those constraints. In most projects the decisive constraint is booth width.
An automatic colour change system is indispensable where different colours run on the line. Changeover time and the amount of paint discarded at each change are the two variables that determine the economics of the system.
Criteria that determine the configuration
Part variety
With few parts of similar geometry the number of programs is small and the investment pays back quickly. With high variety, program management and teaching time become a serious burden.
Safety performance level
The performance level required for each safety function is determined by risk assessment and the circuits are built accordingly. Upgrading later usually means rebuilding the control panel.
Electrostatic suitability
The part must be earthable. In deep recesses and closed sections the Faraday cage effect weakens the coating; additional guns or manual touch-up are planned for these areas.
Operator competence
A robot stands idle without a team that can program and maintain it. Training is an inseparable part of the investment.
Technical framework
| Safety | EN ISO 13849-1 compliant, with performance level calculation |
|---|---|
| Integration | Brownfield (existing line) · greenfield (new plant) |
| Colour change | Automatic colour change system option |
| Application | Electrostatic · conventional |
The figures are typical operating ranges for the sector. Every line is recalculated according to part geometry, target capacity, paint system and customer specification.
Related topics
Let’s arrange a preliminary technical discussion for robotic painting automation. Share your part dimensions, target capacity and paint system, and our process engineer will prepare an outline concept and budget range.