
Surface Treatment and Cataphoresis
Most of a coating’s life is decided not in the paint booth but on the surface treatment line before it. On a part left with an oil film, with irregular phosphate crystals or insufficiently rinsed, even the best paint will not adhere. Cataphoresis follows this preparation: a dip coating applied by electrical charge that reaches recesses and protrusions equally.
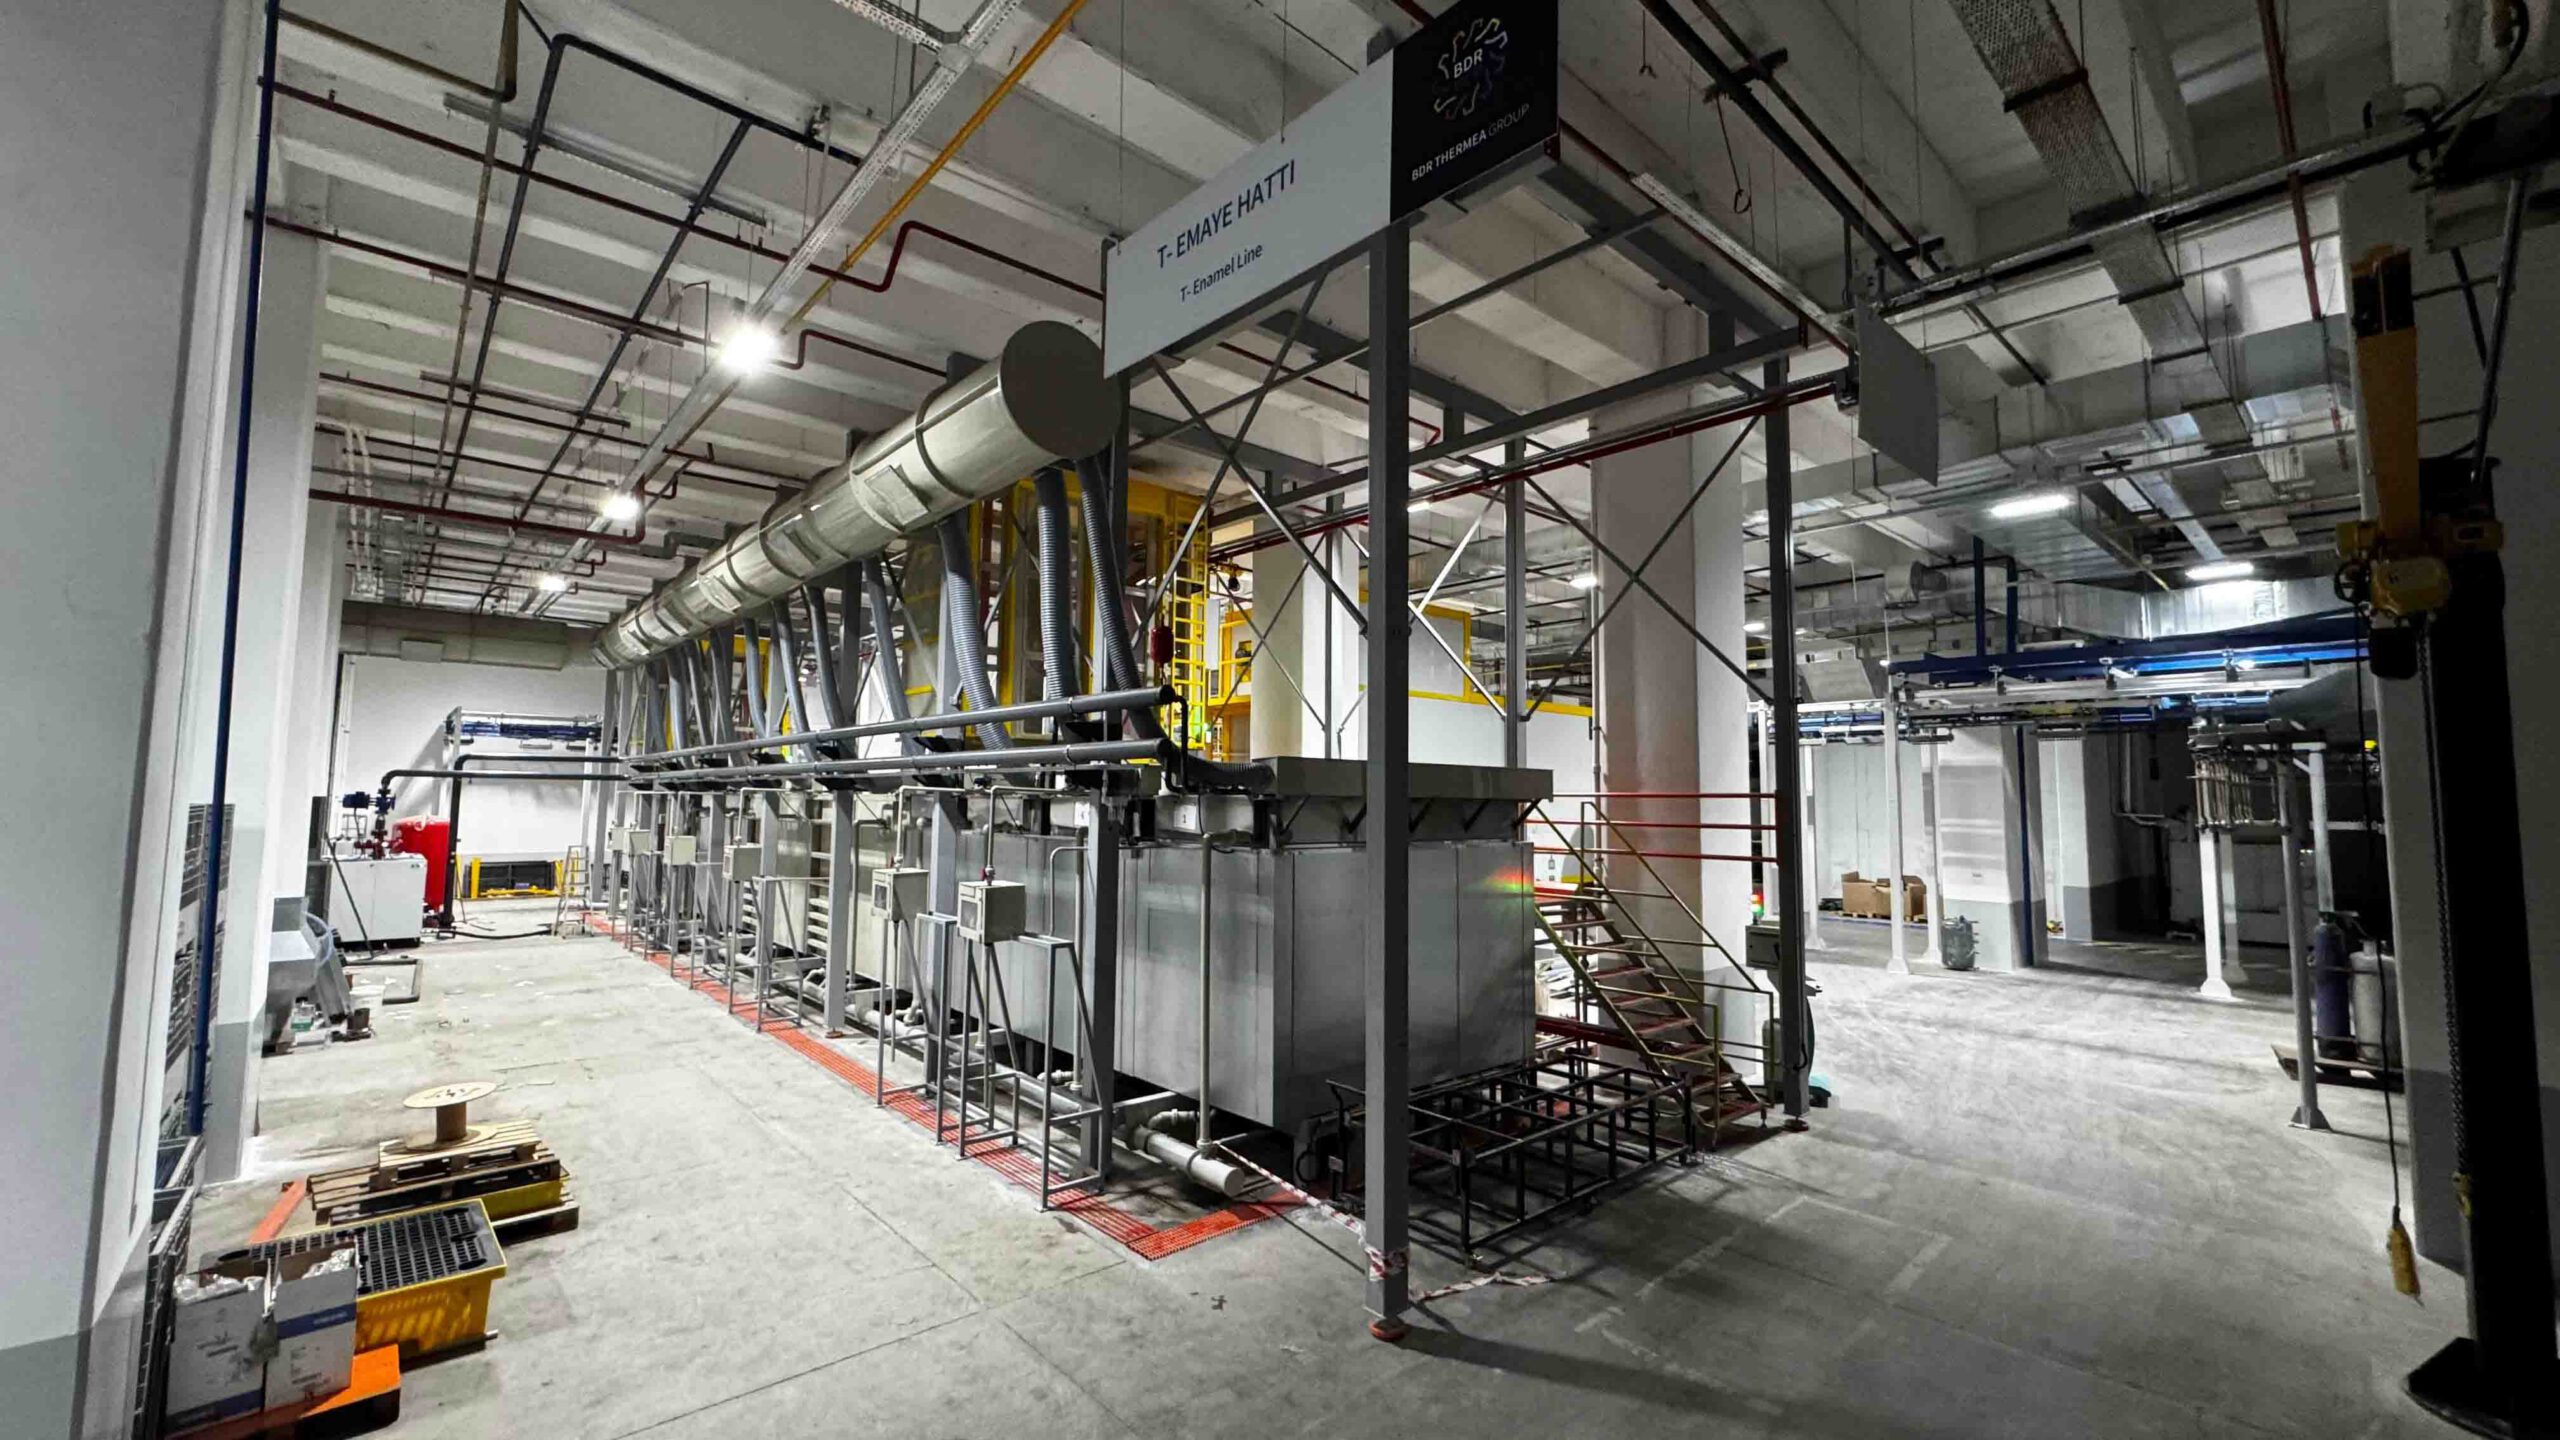
How the process works
The surface treatment line works in stages: degreasing removes drawing oil and soiling from production, activation creates the nucleation points for the phosphate crystal, phosphating grows the crystal structure to which the paint will adhere, passivation seals the crystal, and finally deionised water rinsing brings conductivity below the target value.
At the cataphoresis stage the part becomes the cathode and the resin particles in the bath migrate to the surface under the electric field. As the film thickens, resistance rises, current moves away from that area and the coating is directed to areas still thin. This is the mechanism that carries the coating into box sections, weld pockets and shaded areas; it cannot be achieved by spraying.
After cataphoresis, ultrafiltration recovers the resin carried out of the bath. This markedly reduces both chemical consumption and wastewater load.
Criteria that determine the configuration
Dip or spray
Where there are box sections, closed profiles and welded bodies, dipping is essential; spray cannot reach those voids. For flat sheet and open geometry a spray line takes up less space and reduces investment and chemical volume.
Number of stages
The higher the corrosion target, the more stages are needed. Light protection can be achieved with 6 stages, whereas automotive body specifications typically call for 9–11.
Phosphate type
Zinc phosphate gives high corrosion resistance but produces sludge and adds treatment load. Nano-ceramic pretreatment generates less waste, operates at low temperature and reduces energy consumption; it is preferred where corrosion expectations are moderate.
DI water conductivity
Final rinse conductivity is a direct indicator of coating quality. High conductivity means salt carried over from the bath remains on the surface; it returns as blisters beneath the coating.
Technical framework
| Process stages | 6–11 stages |
|---|---|
| Application method | Dip · spray · combined |
| Pretreatment options | Zinc phosphate · iron phosphate · nano-ceramic |
| DI rinse | Low conductivity target at final rinse |
| Film thickness (E-coat) | Typically 18–25 µm |
| Recovery | Resin recovery by ultrafiltration |
The figures are typical operating ranges for the sector. Every line is recalculated according to part geometry, target capacity, paint system and customer specification.
Frequently overlooked points in design
- Drainage holes: On a dip line, hole positions must be decided at the design stage so the part traps no air pocket and drains fully from the bath. Adding them later is often impossible.
- Hanger design: The hanger contact point is not coated. It must be placed in an area that is either not visible or not critical for corrosion.
- Bath volume and turnover: A bath sized too small cannot hold chemical balance when capacity increases. Volume should be selected for future capacity, not merely the target one.
- Wastewater infrastructure: Where the phosphate sludge and rinse water will go must be resolved before the line is commissioned.
Related topics
- Industrial Ovens — curing after cataphoresis
- Conveyor Lines — handling systems for dip lines
- Energy and Environmental Management — wastewater and heat recovery
- Automotive — body cataphoresis applications
Let’s arrange a preliminary technical discussion for a surface treatment or cataphoresis line. Share your part dimensions, target capacity and paint system, and our process engineer will prepare an outline concept and budget range.