Industrial Ovens
The oven’s job is not to heat but to hold the temperature–time curve the paint requires at every point of the part . The “20 minutes at 160 °C” stated on the paint data sheet describes the temperature of the metal, not of the oven air — managing the difference between the two is the real subject of oven design.
How the process works
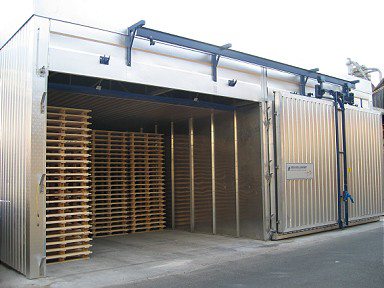
In a convection oven, air is heated in a heat exchanger and blown onto the part through nozzles. Heat is carried by air movement; thick-section parts heat up later than thin ones. On lines with a mixed part flow the oven is therefore sized for the requirement of the thickest part.
IR (infrared) assistance delivers heat directly to the surface and speeds up initial heating. An IR zone placed at the oven entry can shorten total oven length and therefore the building area. However, IR does not reach shaded areas; on complex geometry it is not sufficient on its own.
With solvent-based paints, solvent vapour is released inside the oven. To keep this vapour safely below the lower explosion limit, fresh air is supplied continuously and the exhaust flow is calculated accordingly. EN 1539 defines the framework for this calculation.
Criteria that determine the configuration
Zone deviation
Point-to-point temperature variation within the oven volume causes the coating to cure fully in one area and remain undercured in another. Acceptance testing typically targets ±3 °C, verified by thermal profile measurement.
Heat recovery
When the hot air discharged through the exhaust is used to preheat incoming fresh air, energy consumption falls markedly. This is usually the item with the greatest effect on payback period.
Insulation thickness
Cutting back on insulation lowers the initial investment but costs throughout operation. Panel thickness should be chosen according to operating temperature and daily running hours.
Entry and exit curtains
Hot air escaping from the oven opening is both an energy loss and a disturbance to the surrounding working environment. An air curtain or labyrinth entry limits this loss.
Technical framework
| Operating range | 60–250 °C |
|---|---|
| Zone deviation | ±3 °C |
| Heating method | Convection · IR-assisted · combined |
| Fuel / energy | Natural gas · electricity · thermal oil |
| Heat recovery | Exhaust–fresh air heat exchanger |
| Compliance | EN 1539 |
The figures are typical operating ranges for the sector. Every line is recalculated according to part geometry, target capacity, paint system and customer specification.
Frequently overlooked points in design
- Thermal profile measurement: At acceptance, the actual metal temperature should be measured with data loggers attached to the part. Looking only at oven air temperature is misleading.
- Conveyor thermal expansion: The conveyor passing through the oven expands as it heats. Without an allowance for expansion the line is strained and chain life is shortened.
- Stack measurement point: The straight duct run and measurement port required for emissions measurement must be provided during stack fabrication.
Related topics
Let’s arrange a preliminary technical discussion for a drying or curing oven. Share your part dimensions, target capacity and paint system, and our process engineer will prepare an outline concept and budget range.