
Paint Kitchen
The paint kitchen is the supply centre of the line. The consistency of coating quality achieved in the booth can be no better than the consistency of mixing, temperature and viscosity control here.
What a paint kitchen is
A paint kitchen is a separate room where paint is prepared, mixed, adjusted for viscosity and delivered to the application points through a circulation loop. It is the smallest part of a paint shop, yet it directly determines colour consistency, film thickness and consumption.
When solvent-borne paints are used, this room falls under explosive atmosphere classification. Equipment selection, ventilation design and electrical installation follow that classification. It cannot be retrofitted afterwards; it is built correctly from the start.
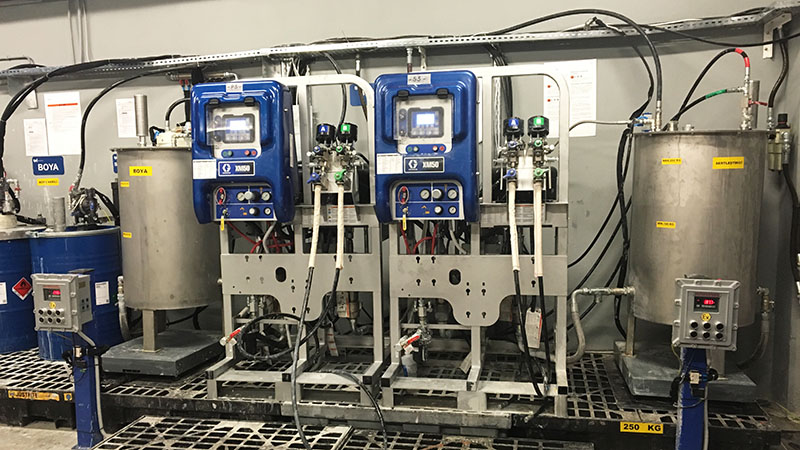
Technical scope
The values below are typical design ranges for kitchens handling solvent-borne paint. Final figures are engineered according to the paint system, consumption rate and the zone classification of the plant.
| Tank volume | 50 – 2,000 L, according to consumption |
|---|---|
| Agitator | Pneumatically driven, 30 – 200 rpm, adjustable |
| Temperature control | 20 – 25 °C, jacketed tank or heat exchanger |
| Relative humidity | 50 – 65 % |
| Viscosity tolerance | ± 3 – 5 % (with in-line measurement) |
| Circulation pressure | 2 – 6 bar, with back-pressure regulator |
| Line flow velocity | 0.3 – 1.0 m/s (between settling and air entrainment) |
| Filtration | 100 – 200 mesh, two stages |
| Ventilation | 10 – 30 air changes per hour, low-level extraction |
| Zone classification | Zone 1 around the tank, Zone 2 for the room |
| Earthing | Continuity across all conductive parts, resistance < 10 Ω |
| Flooring | Conductive, non-sparking finish |
How the process works
Without continuous stirring, pigment settles and the colour drifts within a shift. Agitator speed is also critical: too little stirring fails to prevent settling, too much entrains air in some paints.
The circulation loop carries paint from the kitchen to the guns and returns what is not used. Pressure and flow velocity must be maintained along the loop; in dead zones the paint stalls and dries.
Viscosity is temperature-sensitive. Paint that cools in winter goes on thick, and thins in summer. In kitchens without temperature control, seasonal differences in colour and thickness are a frequent complaint.
A colour change requires the line to be flushed. Flushing time and solvent consumption are set by the volume and layout of the loop. In plants running many colours, a separate circuit is both faster and cheaper than continually flushing a single one.
Explosive atmosphere and safety
Solvent vapour is heavier than air and accumulates at floor level. Extraction is therefore taken from low level, not from above. Ventilation runs not only for occupational health but to keep vapour concentration below the lower explosive limit.
- Agitators are pneumatic — an electric motor introduces an ignition source.
- Static electricity is the principal risk. Flowing paint builds charge through friction; tank, pump, line and drum are bonded to each other and to earth.
- Lighting and sockets are certified equipment matching the zone classification.
- Ventilation failure is interlocked to stop supply; the interlock is monitored by the PLC.
Circulation loop or single-point feed
There are two basic arrangements, and the choice follows consumption rate.
| Circulation loop | Single-point feed | |
|---|---|---|
| Suits | Continuous production, high consumption | Low consumption, frequent colour changes |
| Paint stability | High — the paint never stands still | Risk of settling when idle |
| Colour change | Requires line flushing | Fast |
| Investment | High | Low |
Plants running many colours usually install both: high-volume base colours on a circulation loop, low-volume special colours on single-point feed.
Standards applied
- ATEX 2014/34/EU — equipment and protective systems for use in explosive atmospheres
- EN 60079-10-1 — classification of areas with explosive gas atmospheres
- EN 12215 — safety requirements for coating plants
- EN 1127-1 — explosion prevention and protection; basic concepts and methodology
Frequently asked questions
Does the paint kitchen need to be in a separate room?
With solvent-borne paints, yes. A separate room confines the zone classification: explosive atmosphere measures apply only there, while the rest of the production area stays unclassified. Working in a shared space brings the whole area into classification and multiplies the cost.
Why must viscosity be measured continuously?
Viscosity sets film thickness, and film thickness sets both appearance and corrosion resistance. Measuring once at the start of a shift does not capture the ambient temperature changing through the day. In-line measurement allows correction before the deviation grows.
Can it be added to an existing paint shop?
It can. What decides the case is whether a suitable volume can be separated off and whether there is access to an outside wall for ventilation. The routing of the circulation loop to the booths is also planned at an early stage.
Do the same measures apply to waterborne paint?
Explosive atmosphere measures ease considerably, but the need for a kitchen does not disappear. Waterborne paints are more sensitive to temperature and humidity, so the air conditioning requirement increases. Line materials are also selected differently because of corrosion risk.
Related topics
- Paint Booths
- PLC Automation and Electrical
- Ventilation and Air Conditioning
- Painting Robots
- Industrial Paint Shop Plants
Let’s arrange a preliminary technical discussion for a paint kitchen. Share your paint system, daily consumption rate and number of colours, and our process engineer will prepare an outline concept and budget range. Go to the quote form · Contact channels